Our Core Competencies
We leverage cutting-edge technology and stringent quality control to deliver high-performance medical products to over 48 countries.
Medical Devices
High-precision diagnostic equipment, blood pressure systems, and life-support accessories rigorously tested for clinical accuracy.
Pharmaceuticals
WHO-GMP certified production of oral solid dosages, life-saving injectables, and active pharmaceutical ingredients (APIs).
Hospital Furniture
Ergonomic, durable, and modular hospital beds, OT tables, and ward furniture designed for patient comfort and caregiver efficiency.
Global CDMO
Turnkey contract manufacturing and OEM services, providing seamless production, packaging, and regulatory filing support.
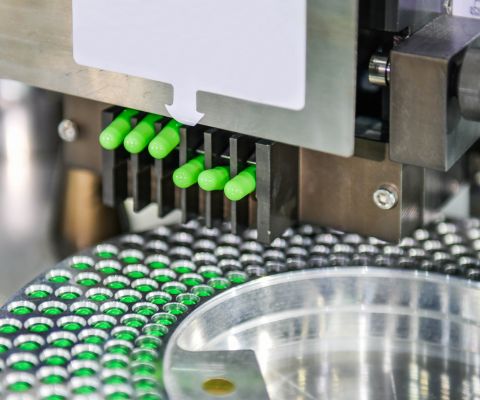
State-of-the-Art Manufacturing Hubs
Our expansive manufacturing facilities are designed to handle high-volume production without compromising on micro-level precision. Equipped with automated assembly lines and Class 100 cleanrooms, we ensure zero cross-contamination and absolute sterility.
- Advanced HVAC Systems: Maintaining stringent air quality and environmental control for sterile formulations.
- Automated Blister Packaging: High-speed Alu-Alu and blister lines ensuring product stability and extended shelf life.
- Device Assembly Zones: ESD-safe areas dedicated to the precise assembly of sensitive diagnostic electronics.
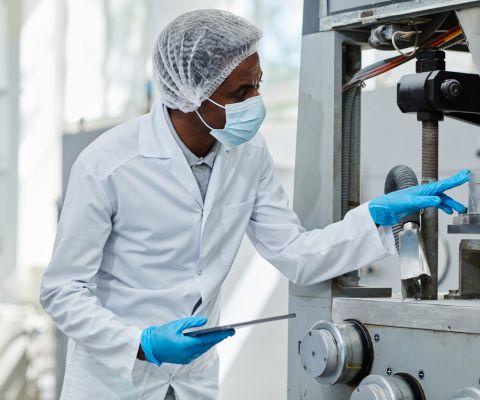
Rigorous Testing & Validation
Quality is the cornerstone of Dr. Tycure. Our independent Quality Control (QC) and Microbiology laboratories are equipped with the latest analytical instruments to validate every batch from raw material to finished product.
HPLC & GC Analysis
Ensuring 99.9% purity and accurate API concentrations.
Regulatory Dossiers
Complete eCTD Module 3 CMC documentation support.
Leverage Our Capabilities for Your Brand
Whether you need white-label manufacturing for medical devices or large-scale formulation of pharmaceuticals, our institutional desk is ready to provide customized quotation and regulatory support.